
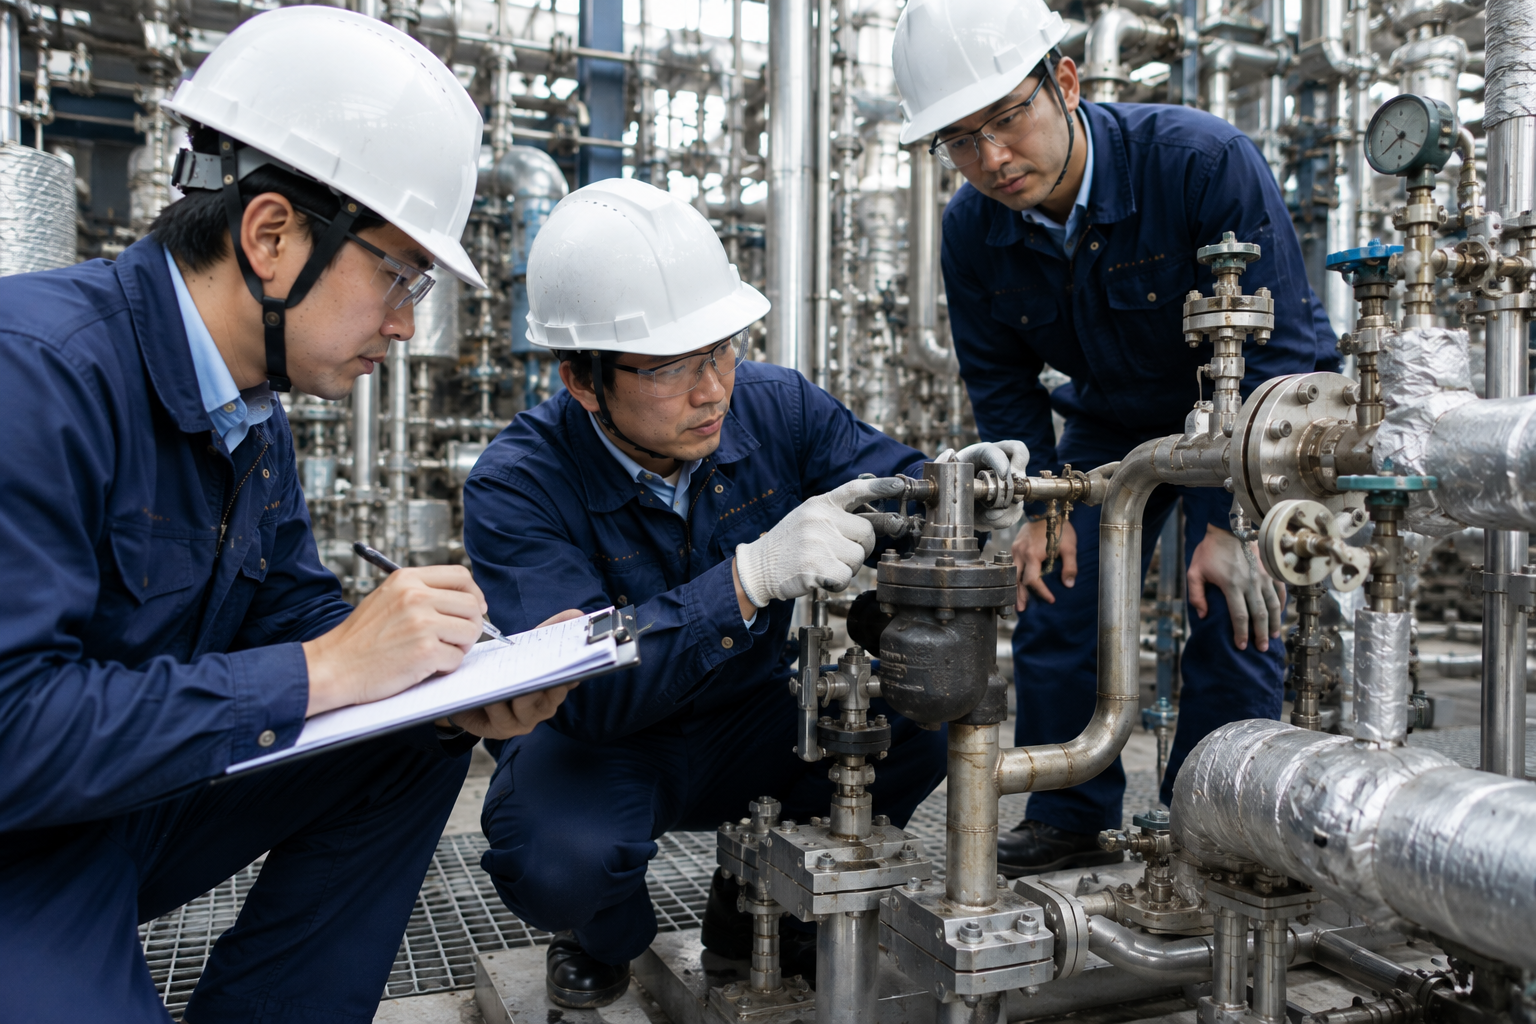
The right inspection interval for a steam trap varies with the operating pressure, frequency of use, trap type, and installation environment, so it cannot be fixed uniformly. A practical approach is to first set an interval, run periodic diagnostics on that cycle, and then adjust the interval while watching how failures emerge. Trap failures progress quietly: a trap can fail open, letting steam leak continuously, or fail closed, so that condensate is not discharged and accumulates. Neither is easy to notice from the outside. Left unattended, wasted steam and insufficient heating add up, so catching the warning signs and replacing traps early is the key to limiting losses. This article organizes how to think about inspection intervals and how to judge replacement timing, in the order they arise in practice.
Key points of this article
- Inspection intervals are not uniform. It is practical to set them according to operating conditions and adjust the interval while continuing periodic diagnostics.
- Because failures are hard to spot visually, judge by combining warning signs in operating sound, temperature, and discharge condition with a dedicated diagnostic instrument.
- Reviewing the surrounding design at the same time as replacement (condensate pockets, dirt pockets, and stall countermeasures) makes it easier to prevent recurrence.
Why steam traps need inspection, and how to think about inspection intervals
A steam trap is a valve that discharges only the condensate collecting in steam piping and equipment while keeping the steam from escaping. There are several types, such as disc, float, and bucket, but the aim is common to all: retain the steam and discard the moisture. When this separation breaks down, it leads to insufficient heating, temperature unevenness, or leakage of the steam itself. Inspection to maintain proper condition therefore ties directly to energy saving and stable operation.
Set inspection intervals according to operating conditions
The rate of deterioration changes with steam pressure, frequency of use, trap type, and installation environment, so the inspection interval cannot be fixed uniformly. Traps used under harsher conditions tend to deteriorate faster and require shorter intervals. A common approach is to tentatively set an interval, run periodic diagnostics on that cycle, and adjust the interval while watching how failures emerge. It is efficient to apply the effort where it matters: shorter intervals for traps on high-importance equipment, and longer ones for lightly loaded locations.
Continuing periodic diagnostics makes it easier to keep the failure rate at a low level. At one chemical manufacturing site, it has been reported that continuing annual diagnostics gradually brought down a failure rate that had initially been high. However, results vary with operation and conditions, so please treat this only as a rough guide.
Signs of failure that are hard to spot visually
Trap failures progress quietly and are hard to notice just by looking from the outside. In daily inspection, useful clues include abnormal operating sound, steam blowing continuously from the discharge outlet, or conversely, condensate accumulating because it is not being discharged and the temperature upstream dropping as a result. Because judgment by feel alone has its limits, combining it with the diagnostic instrument described below improves accuracy.
How to judge replacement timing
A trap judged defective during inspection should be replaced early rather than put off. A trap failed open and leaking steam wastes more energy the longer it is left, while a trap failed closed that cannot discharge can lead to insufficient heating and quality defects.
Judging fail-open vs. fail-closed and using a diagnostic instrument
A dedicated diagnostic instrument is helpful for grasping the operating condition objectively. Using an instrument such as Yoshitake’s steam trap diagnostic instrument STC-1 makes it easier to estimate a fail-open or fail-closed condition from the operating sound and temperature. Furthermore, if you remotely manage the data from traps and flow meters across the plant in one place with a system such as the Wi-Flo fluid monitoring system, you can advance data-based predictive maintenance with a small start, without relying entirely on manual patrols.
Review the surrounding design when replacing
If a trap reverts to a defective condition soon after being replaced with a sound one, the cause may lie not in the trap itself but in the surrounding design. Shortcomings such as an undersized condensate pocket or the absence of a dirt pocket are conditions that tend to shorten service life. In addition, at locations where a stall phenomenon occurs in which condensate stagnates at low pressure, measures such as installing an assist trap are used. Checking these surrounding conditions together when you replace a trap makes it easier to prevent recurrence.
Frequently asked questions
Q1. What does a steam trap do as a valve?
A1. It is a valve that discharges only the condensate collecting in steam piping and equipment while keeping the steam from escaping. It separates steam from moisture and serves the role of using steam without waste.
Q2. What happens when a trap fails?
A2. If it sticks open, steam keeps leaking; if it sticks closed, condensate accumulates. The former tends to waste energy, and the latter tends to cause insufficient heating.
Q3. How often should inspection be performed?
A3. It cannot be fixed uniformly. Because the rate of deterioration changes with pressure, frequency, type, and environment, it is practical to set an interval, run periodic diagnostics, and adjust it while watching how failures emerge.
Q4. Can failure be identified visually?
A4. It is characteristically hard to identify. Because it progresses quietly, pay attention to warning signs in operating sound, temperature, and discharge condition, and using a dedicated diagnostic instrument alongside them makes judgment easier.
Q5. Isn’t the loss from just one leak small?
A5. A single one may be small, but when a plant has many traps, they add up. The cumulative total of defects can become a non-negligible waste of steam, so leaving them unattended tends to lead to losses.
Q6. Why does a trap fail again after being replaced?
A6. The cause may lie in the surrounding design. Examples include an undersized condensate pocket, the absence of a dirt pocket, and the stall phenomenon. We recommend reviewing the surrounding conditions rather than the trap alone.
Q7. How can inspection be connected to energy-saving activities?
A7. The starting point is first reducing the trap failures at your feet. Expanding from there to condensate recovery and waste-heat utilization tends to connect to energy saving across the entire steam system.
Summary
Because their failures progress quietly, steam trap inspections tend to be put off, and this is an area where losses easily accumulate. Set the inspection interval according to operating conditions; capture problems by combining warning signs in operating sound, temperature, and discharge condition with a diagnostic instrument; replace early any trap judged to have failed open or closed; and review the surrounding design at the same time. Keeping this flow in mind makes it easier to hold down both wasted steam and insufficient heating.
If you have concerns such as “we can’t judge how to set the inspection interval,” “there are warning signs but we can’t tell whether it’s fail-open or fail-closed,” or “we have locations that revert to defective soon after being replaced with sound traps,” please organize the conditions and make use of Yoshitake’s technical and selection consultation. Based on your operating pressure, flow rate, and installation environment, we will consider together how to proceed with inspection and replacement and how to review the surrounding design.