
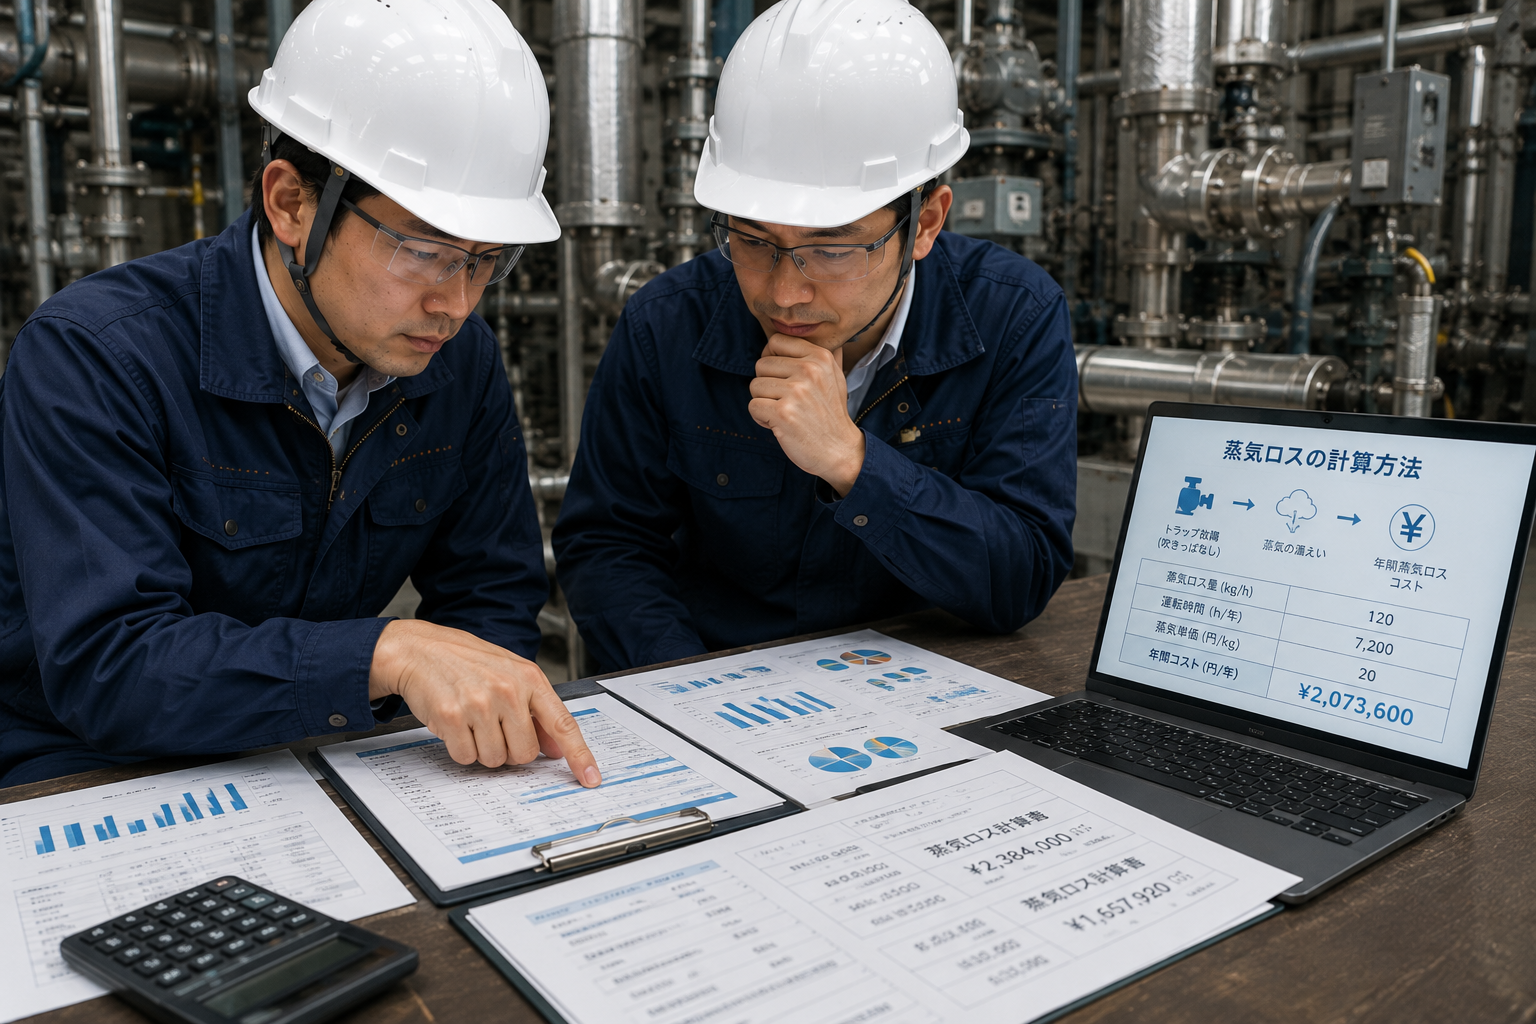
When a steam trap fails and lets steam blow through, the loss can be roughly estimated as an annual cost using the formula “steam leakage rate (kg/h) × operating hours × unit price of steam.” The first thing to grasp is the leakage rate per failed trap. By deriving the theoretical leakage rate from the orifice diameter and pressure, and multiplying it by the operating hours and the fuel-based unit price of steam, a loss on the order of tens of thousands to hundreds of thousands of yen per year per trap becomes visible as a concrete figure. Capturing this through calculation rather than intuition is the starting point for prioritizing inspection and replacement.
Key points of this article
Steam loss can be roughly estimated as “leakage rate × operating hours × unit price of steam,” and the orifice diameter and pressure govern the leakage rate. The figures are only a guide; because actual losses vary with the failure mode (blow-through or blockage) and piping conditions, they should be used in combination with field measurements.
The concept behind converting steam loss into a monetary figure
A steam trap normally discharges only condensate while blocking steam. When it fails and stays open (blow-through), steam is discharged out of the system as is, producing a loss that directly translates into fuel cost.
Estimating the leakage rate (orifice diameter and pressure)
The blow-through leakage rate is determined by the diameter of the orifice (valve seat) inside the trap and the differential pressure across it. In general, the larger the orifice diameter and the higher the steam pressure, the greater the leakage rate. Theoretically it can be roughly estimated using the nozzle discharge equation, but in practice it varies with the degree of valve seat wear and partial opening, so the value obtained should be regarded as “a guide close to the upper limit.”
For example, even a small-diameter orifice can, depending on conditions, produce a leak of several kg/h or more with medium-pressure-class steam. If multiple traps have failed at the same time, their combined total reaches a scale that cannot be ignored.
Multiplying the unit price of steam by the operating hours
Once the leakage rate is determined, multiply it by the operating hours and the unit price of steam. The unit price of steam is calculated from the fuel type of the boiler in use (city gas, heavy oil, electricity, etc.), the boiler efficiency, the feedwater temperature, and so on, and it differs from one site to another. If your own actual value is available, use it; if not, use in-house cost data or an estimate from the utility department.
Annual loss (yen) = leakage rate (kg/h) × annual operating hours (h) × unit price of steam (yen/kg). Although this is a simple formula, matching the operating hours to the actual situation governs the accuracy. Because the result changes greatly depending on whether the operation is continuous or intermittent, give priority to actual data here.
Connecting the figures to inspection and replacement decisions
The point of the calculated result is not merely to grasp the amount of loss, but to make it material for inspection intervals and replacement decisions.
Differences in loss by failure mode
Trap failures fall broadly into “blow-through (fail-open)” and “blockage (fail-closed).” The one that matters from the standpoint of loss cost is mainly blow-through, but blockage can cause water hammer due to condensate accumulation, reduced thermal efficiency, and effects on product quality, entailing secondary damage that is hard to capture in a cost calculation. Monetary conversion is only a guide centered on blow-through, and blockage risk needs to be evaluated on a separate axis.
Prioritization and replacement planning
When replacing all traps at once is difficult, prioritizing inspection and replacement of traps with larger diameters, higher pressures, and longer operating hours makes it easier to raise the return on investment. Traps whose annual loss exceeds the replacement cost are candidates for which the replacement can be expected to pay for itself. However, the estimate is only an approximation, and we recommend making the actual decision in combination with on-site leakage measurement (ultrasonic diagnosis, temperature measurement, etc.).
Frequently asked questions
Q1. How can I find out the leakage rate?
A1. A guide value can be obtained through theoretical calculation from the orifice diameter and pressure. For greater accuracy, combine this with on-site measurement such as ultrasonic diagnosis or surface temperature measurement.
Q2. I don’t know the unit price of steam within our company.
A2. It is calculated from the boiler’s fuel type, efficiency, and feedwater temperature, but in many cases the utility department or the cost management department holds an estimated value. We recommend first checking in-house data.
Q3. Is there any point in calculating even a small leak?
A3. Even if the amount per trap is small, the total tends to become large when multiplied by the number of units and the annual operating hours. Getting an overall view in monetary terms makes priorities clear.
Q4. Can losses on the blockage side be calculated?
A4. Blockage mainly involves secondary damage such as reduced thermal efficiency and effects on quality, so it is not suited to simple monetary conversion. It is common to evaluate the risk from a perspective different from blow-through.
Q5. Can the calculated result be used directly as grounds for replacement?
A5. It is useful as an approximation, but because it varies greatly with conditions, make the decision in combination with actual measured values. It is appropriate to position the estimate as the starting point for prioritization.
Q6. Which traps should be reviewed first?
A6. In general, traps with larger diameters, higher pressures, and continuous operation tend to incur greater losses, so inspecting those first tends to make it easier to obtain results.
Summary
Steam loss can be roughly estimated as “leakage rate × operating hours × unit price of steam,” and the orifice diameter, pressure, and operating conditions govern the result. Treating the figures as a guide and using them, together with on-site measurement, to prioritize inspection and replacement leads to reasonable cost reduction.
If you find yourself thinking “we can’t estimate our annual loss because we don’t know our steam unit price,” “we’ve done the theoretical leakage calculation but are unsure which traps to replace,” or “we want to select an equivalent product for an existing trap,” please organize the conditions and consult Yoshitake. Based on conditions such as operating pressure, diameter, and operating hours, we will provide technical proposals on appropriate trap selection and the approach to replacement.